Aboveground Atmospheric Storage Tanks

Emptying and cleaning a 50-meter crude or chemical storage tank for internal inspection costs between €300,000 and €500,000, while taking the asset out of service for up to 90 days. Over 75% of tanks opened on calendar intervals require zero major repair.

Updem delivers continuous in-service integrity monitoring from the tank perimeter without taking assets out of service:

  • Bottom Plate Pitting Detection: Distinguishes active corrosion pitting from background tank settling noise.
  • Annular Ring Weld Surveillance: Monitors the critical shell-to-bottom weld joint for cyclic fatigue during filling and emptying cycles.
  • Foundation Settlement Tracking: Warns when uneven ground movement exerts high localized bending moments on the lower shell strakes.
Request Storage Tank Pilot Study →
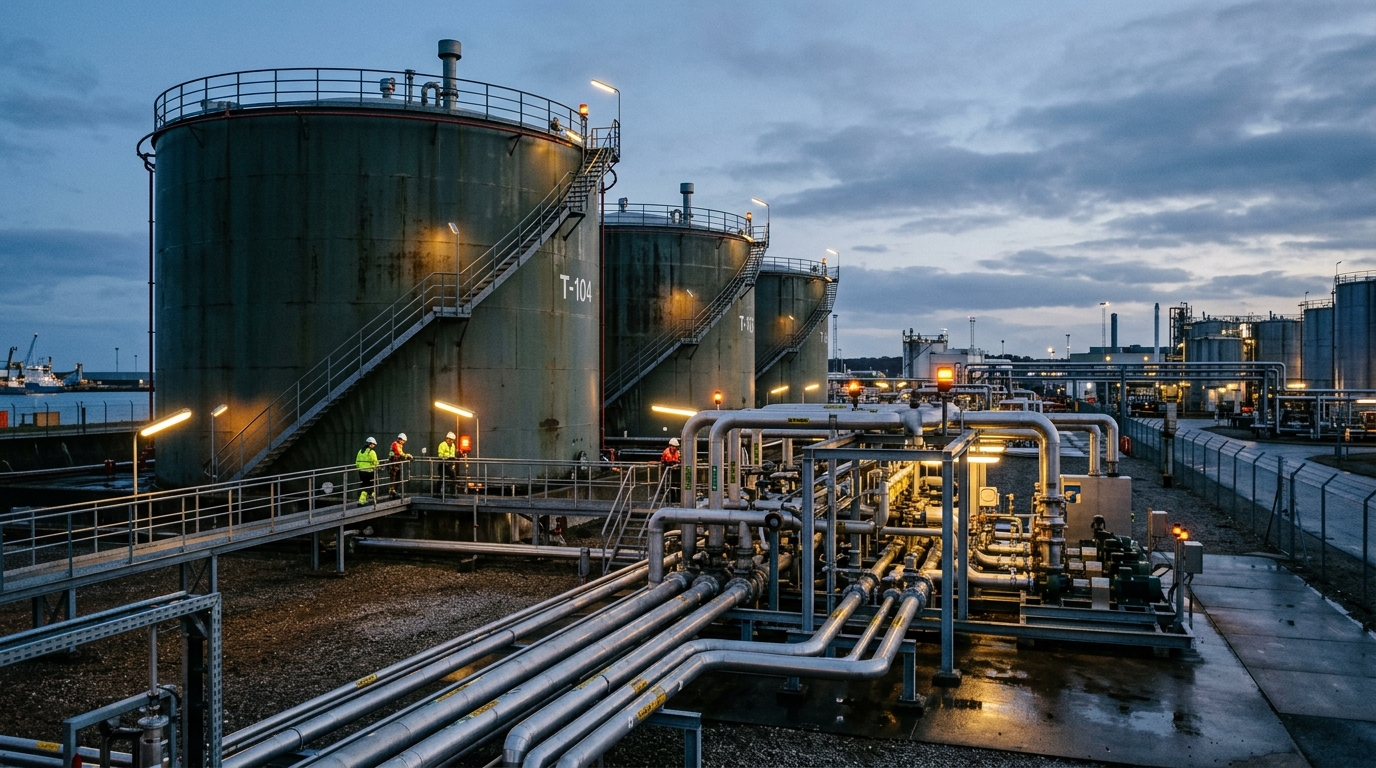
Atmospheric storage tanks monitored by Updem
API 653: Continuous acoustic listening eliminates blindspots between 10-year turnarounds.

Heavy Wall Pressure Reactors & Columns

In hydro-processing, catalytic cracking, and chemical synthesis, thick-walled vessels operate under extreme thermal transients and hydrogen partial pressure. Hydrogen-Induced Cracking (HIC) and Stress-Corrosion Cracking (SCC) can advance rapidly between turnaround windows.

Updem's high-temperature acoustic waveguides transmit acoustic stress waves safely outside thermal insulation blankets:

  • Operating temperatures up to 500°C: Solid metal waveguides isolate sensors from extreme vessel surface heat.
  • Micro-crack incubation tracking: Detects elastic energy pulses from dislocation pileups weeks before macroscopic cracking occurs.
  • Thermal shock correlation: Correlates acoustic burst clusters with plant process historians to identify operational practices accelerating equipment fatigue.
Request Reactor Surveillance Specs →
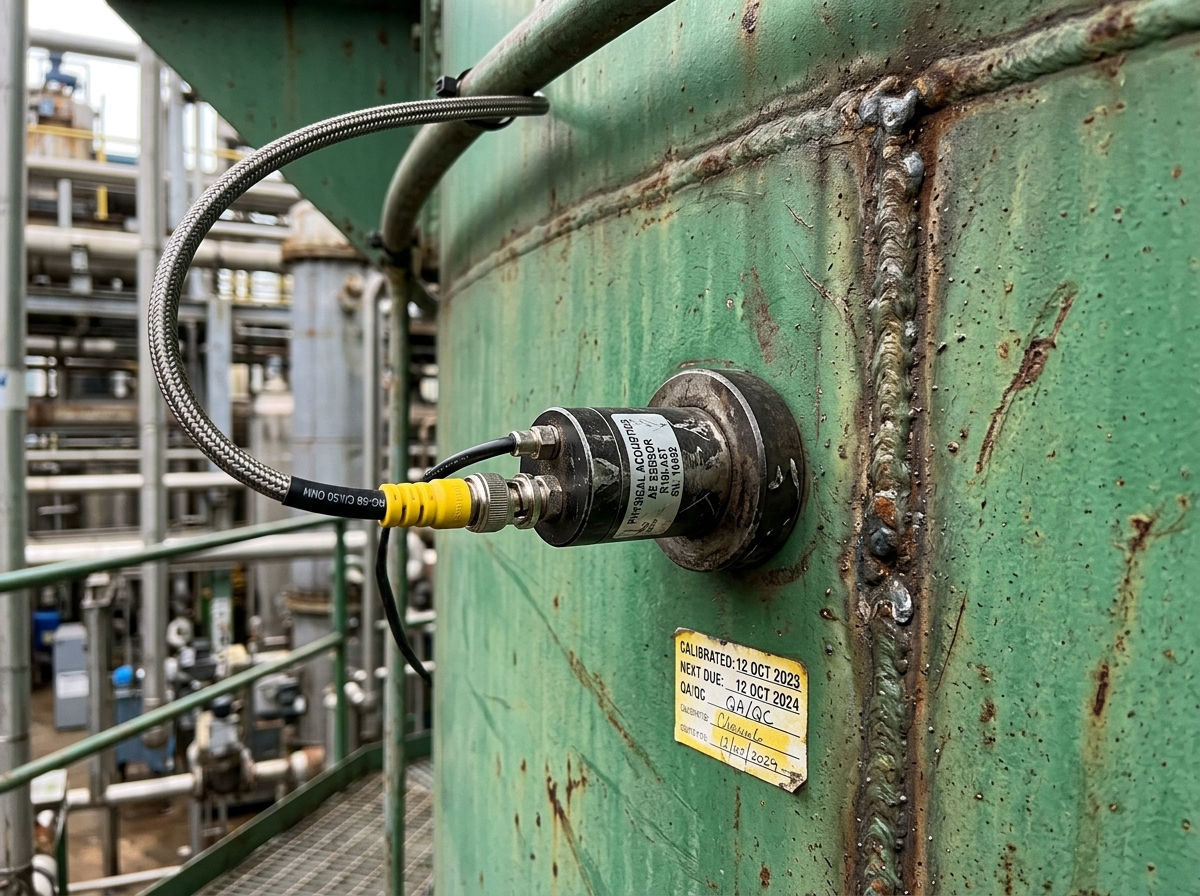
Acoustic sensor mounted on high-pressure vessel shell
WAVEGUIDE INTEGRATION: Monitoring heavy wall reactors without stripping insulated cladding.

Critical Transfer Manifolds & Steam Headers

High-temperature main steam lines in thermal power plants and cross-facility chemical transfer manifolds cannot accommodate regular pigging or internal tools. Weld creep cracking and pressure surge fatigue represent major catastrophic safety threats.

  • Pinpoint Acoustic Leak Detection: Continuous acoustic noise profiling detects pressurized micro-leaks (gaseous or liquid) as small as 0.05 L/min long before perimeter gas sensors trigger.
  • Steam Header Creep Monitoring: Continuous acoustic monitoring of P91 / P22 chrome-moly alloy welds during cyclic thermal ramp-up.
  • ATEX Zone 0 / 1 Architecture: Intrinsically safe sensor barriers safe for explosive atmospheric zones.
Request Piping Integrity Assessment →
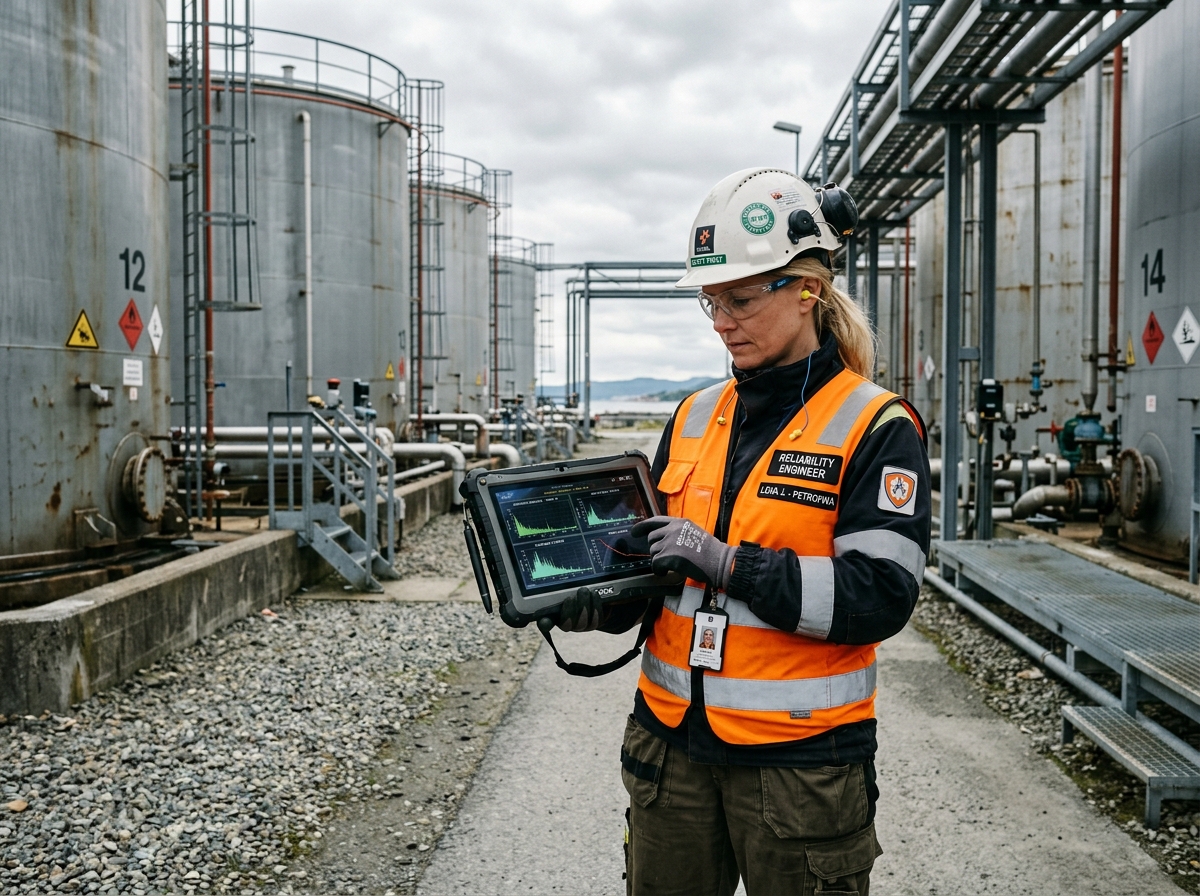
Engineer inspecting industrial piping manifold
PIPELINE MONITORING: Zone-synchronized transducers along manifold sections.
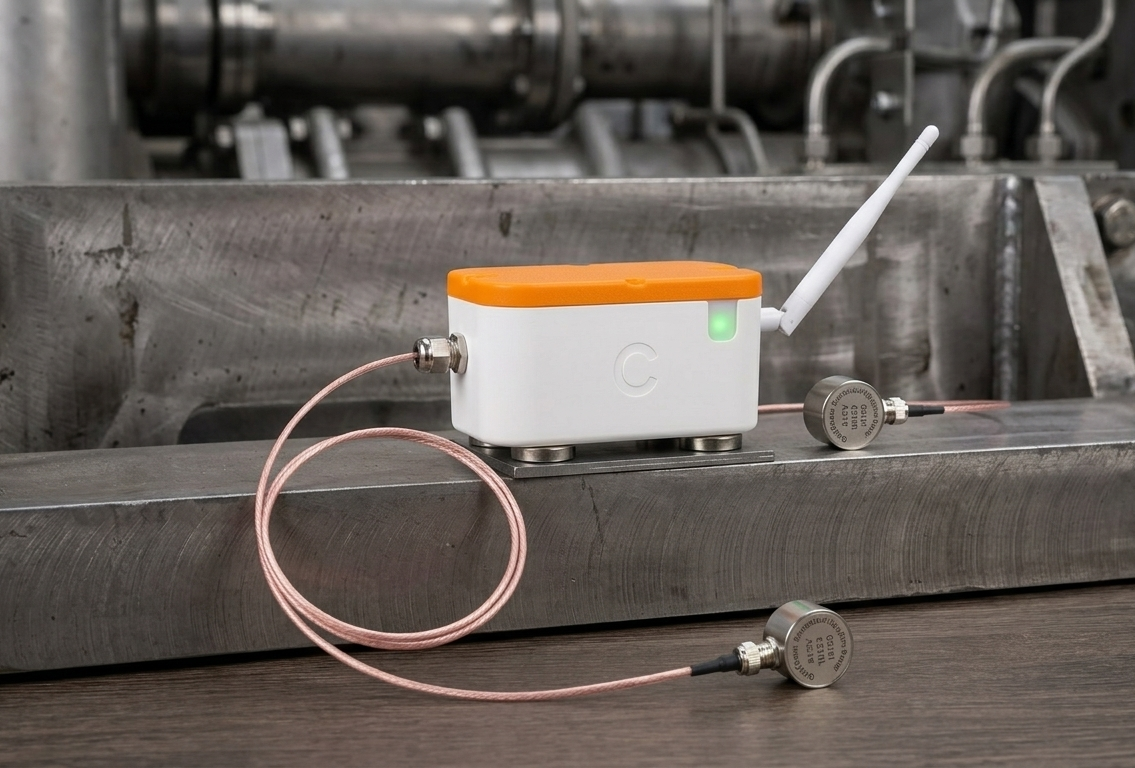
Updem Monpod wireless acoustic emission hardware module
RAPID DEPLOYMENT: Monpod wireless module attaches magnetically to static steel assets with zero hot work permits.

Autonomous Monpod™ Modules & Cloud Predictive Intelligence

Deploying acoustic monitoring across large tank farms or pipeline manifolds no longer requires extensive conduit runs or scaffolding.

Each Monpod™ wireless module attaches via high-strength magnetic feet directly to the steel shell. Dual differential piezoelectric transducers listen passively for microscopic fracture energy bursts, while onboard edge processors compute physical parameters.

Data streams securely via MQTT into the Updem Cloud Platform, where dynamic learned baselines track asset degradation trends and surface explainable anomaly alerts before unplanned downtime occurs.

Review System Architecture →

Fits Your Existing Reliability Architecture

Updem does not lock you into a proprietary walled garden. Our cloud platform and edge gateways connect to your existing plant network via secure MQTT, HTTPS, OPC UA, and Modbus TCP.

Beyond acoustic emission, our cloud predictive maintenance platform is protocol-agnostic and ingests third-party sensors including vibration transmitters, temperature probes, line pressure gauges, and ultrasonic thickness meters to give reliability teams a unified asset health picture.

  • Protocol-agnostic cloud ingestion (MQTT, HTTPS, OPC UA, Modbus)
  • Multi-sensor correlation (AE with vibration, pressure, and temperature)
  • SAP Plant Maintenance (PM) and IBM Maximo work order triggers
  • AVEVA / OSIsoft PI historian bidirectional connector
  • On-premise air-gapped deployment option

Frequently Asked Technical Questions

Common technical inquiries from plant reliability superintendents, inspection engineers, and turnaround managers.

No. Updem acoustic transducers mount externally using high-strength magnetic fixtures and acoustic couplants (or non-magnetic strap-clamps for stainless vessels). Zero hot work permits are needed, and installation occurs while the asset operates at full capacity.
Under API 653 Section 6.4.2 and API 581 RBI methodology, continuous integrity surveillance provides empirical health verification that justifies extending internal out-of-service inspection intervals from 10 years to 15 or 20 years, saving millions in turnaround expenses.
Yes. We utilize solid stainless steel acoustic waveguides that penetrate small cladding inspection ports to make direct contact with the steel vessel wall. This allows continuous monitoring of equipment operating up to 500°C without stripping insulation blankets.
Updem edge gateways feature integrated cellular LTE-M / NB-IoT modems with optional satellite uplink, plus solar-powered battery enclosures. For high-security plants, we support fully on-premise, air-gapped Ethernet and Modbus/OPC UA connections.
We filter mechanical noise in both hardware and software. Piezoelectric sensors are resonant between 150 kHz and 300 kHz (far above low-frequency mechanical vibrations), while edge algorithms separate continuous fluid friction from abrupt, high-energy acoustic emission burst transients.

Download the Complete Engineering Specification Datasheet

Detailed technical tolerances, frequency response curves, ATEX Zone 0 safety architecture, and API 653/581 compliance matrix for plant maintenance directors.

UPDEM OY
Industrial Acoustic Sensing Division • Tampere, Finland
DOCUMENT: DS-AE750P-REV4
CLASSIFICATION: TECHNICAL SPECIFICATION
DATE: SEPTEMBER 2026

Updem Monpod™ Wireless Acoustic Emission Module & Cloud Platform

Autonomous wireless acoustic emission hardware module with magnetic mounting feet and cloud predictive maintenance platform for continuous static asset integrity monitoring.

1. Monpod™ Wireless Hardware Specifications

Hardware System Monpod™ Wireless Module: Self-contained autonomous sensor enclosure with magnetic mounting feet and visual diagnostic LED.
Acoustic Transducers Dual differential piezoelectric ceramic transducers with low-noise balanced preamplification.
Acoustic Frequency Bandwidth 100 kHz to 1 MHz ultrasound passband (tuned to reject plant mechanical rumble).
Edge Feature Extraction Onboard real-time computation of MARSE energy, peak amplitude, duration, hit count, and RMS.
Dynamic Range 15 dBAE to 105 dBAE (Linear response > 90 dB).
Continuous Sampling Rate Up to 1 MS/s transient acoustic capture at the edge.
Mounting Method High-pull neodymium magnetic feet for 5-minute clamping onto steel without hot work or shutdowns.
High-Temperature Waveguides Direct surface up to +150°C; up to +550°C using solid 316L stainless acoustic waveguides.
Wireless Telemetry Uplink LoRaWAN and Cellular LTE-M / NB-IoT with MQTT protocol transmission.

2. Cloud Predictive Maintenance Platform Specifications

Cloud Infrastructure High-availability telemetry platform with centralized static asset hierarchy (tanks, reactors, pipelines).
Baseline Learning Engine Autonomous learned operational baseline per asset during steady-state production.
Anomaly Detection Unsupervised statistical and physical feature drift scoring before defect progression.
Alert Explainability Plain-language engineering directives detailing exact feature deviations (e.g. 4x energy rise over baseline).
Closed-Loop Feedback One-click engineer confirmation loop (confirm / false alarm) continuously training site models.
Standards & CMMS Links API 650/653 Annex C, API 581 RBI, ASME Section VIII, REST API, MQTT, and SAP PM / Maximo connectors.
Engineered by Updem Oy • Platform 6, Tampere, Finland • Tel: +358 46 847 2441